Categories
Fusible Interlining Interlining

What Is the Difference Between Fabric Fusing and Fabric Bonding?

When it comes to garment manufacturing, the way different fabric layers are joined plays an important role in the final look, feel and durability of a garment. You may have come across terms such as fabric fusing and fabric bonding while exploring textile processes. Although these terms are often used interchangeably, they do not mean exactly the same thing.

At Double Ghoda, we work with interlining fabrics and understand how important the right fabric-joining technique is for achieving the desired garment structure. Fabric fusing is a specific process that uses heat-activated adhesive to attach a supporting layer, usually fusible interlining, to the main fabric. Fabric bonding, on the other hand, is a broader term that includes different techniques for joining fabric layers.

Understanding this difference helps you make better decisions about fabric construction, garment structure and material selection. So, let us explore how both processes work and where each one is commonly used.

What Is Fabric Fusing?

Fabric fusing is a process of joining two fabric layers with the help of a heat-activated adhesive. It commonly involves attaching fusible interlining to the reverse side of the main fabric using controlled heat, pressure and time.

The purpose of this process is to give your fabric additional body, stability and shape without requiring extra stitching to attach the supporting layer. It is widely used in garment manufacturing, particularly for components that need to maintain a defined shape, such as collars, cuffs, waistbands and jacket fronts.
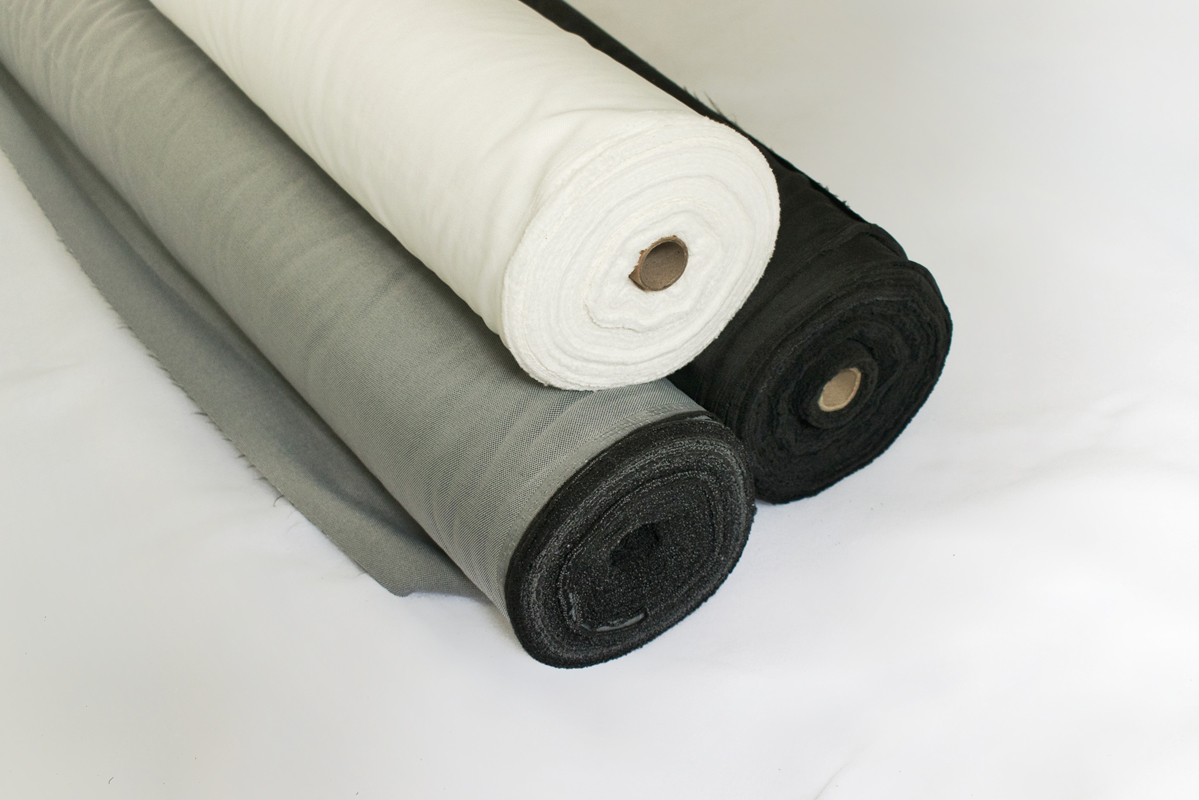
Interlining Fabric

How Does the Fabric Fusing Process Work?

Fabric fusing follows a controlled process to ensure that the interlining attaches properly to the main fabric. Here is how we can understand the process step by step:

  1. Select the fabrics: Choose a suitable main fabric and fusible interlining that are compatible with each other.
  2. Position the layers: Place the adhesive-coated side of the interlining against the wrong side of the main fabric.
  3. Apply heat and pressure: Use a fusing press or suitable equipment to apply the required heat and pressure for a specific duration.
  4. Allow the layers to cool: As the adhesive cools, it solidifies and helps hold both fabric layers together.
  5. Check the finished fabric: Inspect the fused material for even adhesion, bubbles, wrinkles or visible adhesive marks before proceeding with garment production.

The correct temperature, pressure and application time depend on the adhesive and fabric being used. We recommend following the interlining manufacturer’s specifications and testing a sample before bulk production.

What Is Fusing Cloth and How Does It Work?

Fusing cloth is a supporting fabric that has a heat-activated adhesive coating on one side. When you apply it to the main fabric using heat and pressure, the adhesive softens and attaches the two layers.

The adhesive is generally applied in small dots or a thin coating across the surface. During the fusing process, these adhesive points soften and create a connection between the interlining and the main fabric. Once cooled, they help the fabric maintain its added structure and stability.

The adhesive distribution also plays a role in the final fabric feel. A suitable coating can provide support while allowing the fused material to retain flexibility and breathability.

What Is the Role of Fusible Interlining?

Fusible interlining is one of the most commonly used materials in fabric fusing. It acts as a supporting layer that helps your garment maintain its shape and structure.

When attached to the main fabric, it can:

  • Add firmness and body to lightweight fabrics.
  • Prevent fabric edges from stretching or losing their shape.
  • Provide support to collars, cuffs and waistbands.
  • Improve the stability of stitching areas.
  • Help garment components maintain their shape during regular wear and washing.

By selecting suitable fusible interlining, you can achieve the desired balance of softness, flexibility and firmness in your garment.
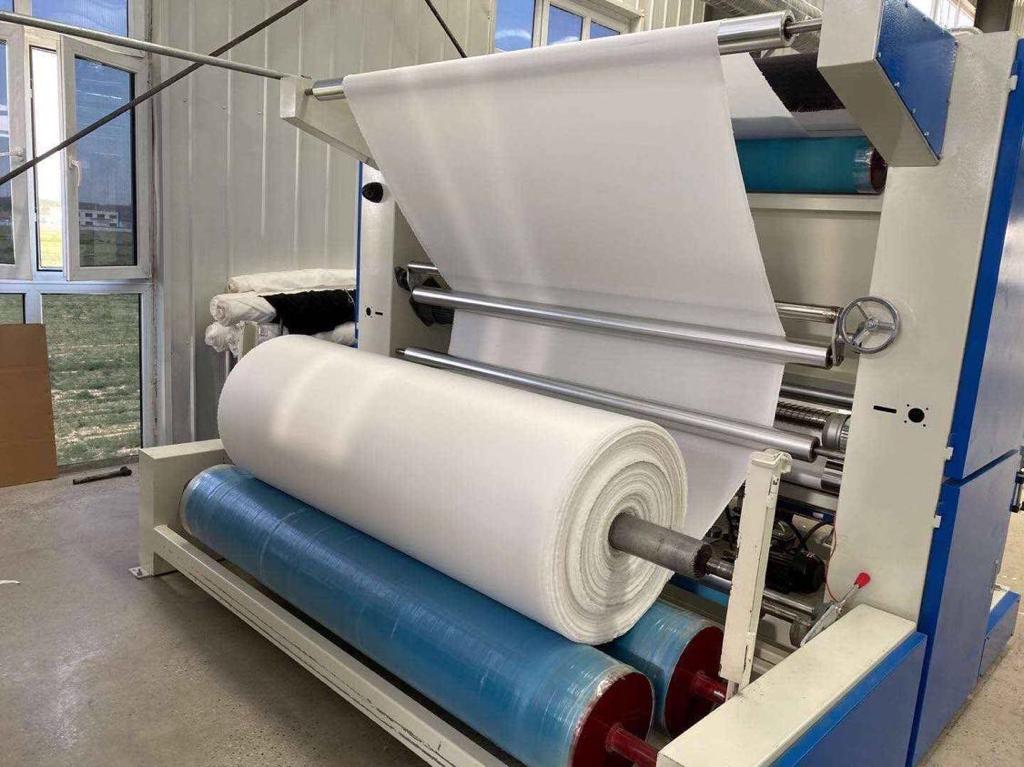
Fusible Interlining

What Is Fabric Bonding?

Fabric bonding is a broader textile process in which two or more fabric layers are joined to function as a single material or component. Unlike fabric fusing, bonding is not limited to heat-activated adhesive or interlining.

Depending on the material and intended application, fabric bonding can involve adhesives, heat or ultrasonic energy. These techniques are used across different industries, including apparel, upholstery, medical textiles and technical textiles.

The main purpose is to combine different layers to achieve specific properties such as strength, flexibility, insulation, water resistance or a particular surface finish.

How Does the Fabric Bonding Process Work?

In fabric bonding, two or more layers are attached across their surfaces so they work together as one material. The exact process depends on the bonding technique being used.

For example, a fabric layer may be joined to a waterproof membrane to create a laminated material. Similarly, foam can be attached to fabric to produce a cushioned or padded textile structure.

The choice of bonding method depends on the type of fibres, material compatibility, intended use and finish you want to achieve.

What Are the Different Methods of Fabric Bonding?

Fabric bonding can be carried out using different techniques. Some of the commonly used methods include:

1. Adhesive Bonding

In this method, a separate adhesive is placed between two fabric layers. It may be in the form of liquid, paste, film or hot-melt web. The layers are then pressed together while the adhesive sets or cures.

We commonly see this method in laminated fabrics and certain technical textile applications.

2. Heat Bonding

Heat bonding uses heat to soften a thermoplastic material present between or within the fabric layers. Once softened, the material helps join the layers together.

Examples include thermal bonding of non-woven fabrics, flame lamination of foam to fabric and the use of fusible webs. Fabric fusing with heat-activated adhesive is closely related to this method.

3. Ultrasonic Bonding

Ultrasonic bonding uses high-frequency vibrations to generate heat at the points where fabric layers meet. This heat softens or melts suitable synthetic fibres, allowing them to join without additional adhesive or sewing thread.

This technique is commonly used for sealed seams, quilting patterns and certain activewear details. It works best with materials containing thermoplastic fibres such as polyester or nylon.

Where Are Bonded Fabrics Commonly Used?

Bonded fabrics are used in several everyday products and specialised textile applications. Some examples include:

  • Waterproof and breathable jackets made with laminated membranes.
  • Foam-backed fabrics used in outerwear, footwear and car interiors.
  • Sportswear and underwear with seamless or taped seams.
  • Disposable medical gowns and hygiene products.
  • Upholstery and filtration materials.

These applications show how fabric bonding can combine different materials to achieve specific performance and functional requirements.

What Is the Difference Between Fabric Fusing and Fabric Bonding?

The main difference between fabric fusing and fabric bonding is their scope and the techniques involved.

Fabric fusing is a specific method of joining a supporting layer to the main fabric using a heat-activated adhesive, generally through fusible interlining. Fabric bonding is a wider category that includes adhesive bonding, heat bonding and ultrasonic bonding.

In simple terms, fabric fusing is one type of fabric bonding, but not every bonding process is fabric fusing.

Difference in Process and Technique

Fabric fusing is generally carried out using a fusing press or suitable heat application equipment. A pre-coated interlining is placed against the main fabric and attached through controlled heat, pressure and time.

Fabric bonding includes several other methods, such as adhesive lamination, thermal bonding and ultrasonic joining. The process varies depending on the materials and the intended result.

Materials Used in Both Methods

For fabric fusing, we generally use the main garment fabric along with woven, knitted or non-woven fusible interlining that has a heat-activated adhesive coating.

Fabric bonding can involve a wider range of materials, including ordinary fabrics, foams, films, membranes, adhesive webs and thermoplastic fibres.

Role of Heat, Pressure and Adhesives

In fabric fusing, heat, pressure and time are essential because they activate and set the adhesive present on the interlining.

However, not every fabric bonding technique requires all three. Some adhesive bonding methods use adhesives that cure without heat, while ultrasonic bonding joins suitable synthetic fibres through vibration-generated heat without requiring additional adhesive.

Applications and Fabric Finish

Fabric fusing is mainly used in garment construction to provide structure and support to specific components. You will commonly find it in collars, cuffs, plackets, waistbands and jacket fronts.

Fabric bonding has wider applications, including laminated outerwear, sealed seams, foam-backed textiles and technical fabrics.

The final finish also varies. A properly fused fabric can retain a soft, tailored feel while providing support. Bonded fabrics may range from flexible to firm, depending on the joining method and materials used.

Fabric Fusing vs. Fabric Bonding: Quick Comparison

AspectFabric FusingFabric Bonding
MeaningA specific fabric-joining methodA broader category of joining methods
Main joining agentHeat-activated adhesive on fusible interliningAdhesives, heat or ultrasonic energy
ProcessPressing under controlled heat and pressureAdhesive lamination, heat bonding or ultrasonic joining
MaterialsMain fabric and fusible interliningFabrics, foams, films, membranes and thermoplastic fibres
Adhesive requirementPre-coated adhesive is requiredDepends on the bonding method
Common applicationsCollars, cuffs, waistbands and jacket frontsLaminated outerwear, sealed seams and technical textiles
Final finishProvides garment shape and supportCan range from flexible to firm, depending on the method

Is Fabric Fusing a Type of Fabric Bonding?

Yes, fabric fusing is a type of fabric bonding. However, the two terms have different meanings in textile manufacturing.

Fabric fusing uses a heat-activated adhesive, generally applied to fusible interlining, to join a supporting layer with the main fabric. Fabric bonding includes this process as well as other techniques such as adhesive lamination, thermal bonding and ultrasonic welding.

Think of fabric bonding as the larger category and fabric fusing as one specific method within it. Every fused fabric is bonded, but not every bonded fabric is fused.

Understanding the Relationship Between Fusing and Bonding

The relationship between these processes becomes clearer when we look at how each one works.

During fusing, the adhesive is already present on the interlining. Heat activates it, pressure helps it attach to the main fabric, and cooling allows the adhesive to set.

In other bonding techniques, the joining process may involve a separate adhesive layer, thermoplastic materials or ultrasonic vibrations. For example, a waterproof jacket made by joining fabric with a membrane is bonded, but it is not necessarily made through the conventional interlining fusing process.

How Does Interlining Fabric Help Us Achieve Better Fusing Results?

Interlining fabric is a supporting layer placed between the outer fabric and the lining of a garment, or attached to specific garment components. It helps improve the structure, stability and overall appearance of the finished garment.

When we use fusible interlining, one side of the material carries a heat-activated adhesive coating. This allows you to attach it to the main fabric through the fusing process.

Choosing the right interlining fabric is important because the weight, construction, adhesive and compatibility with the main fabric all influence the final result.

How Does Fusible Interlining Support Your Main Fabric?

Fusible interlining provides additional support without requiring separate stitching to attach the supporting layer. It helps your main fabric maintain its intended shape and makes garment construction more manageable.

Some of its key functions include:

  • Reducing unwanted stretching along fabric edges.
  • Helping prevent seams from puckering.
  • Providing support to collars, cuffs and waistbands.
  • Improving the stability of areas that require stitching.
  • Helping garment components retain their shape during use.

For the best results, the interlining should be compatible with the main fabric. A lightweight fabric may require a softer interlining, while heavier materials may need a firmer supporting layer.

What Is Body Fusing in Garment Manufacturing?

Body fusing is the process of attaching interlining across the main body panels of a garment, such as the front panels of a jacket or coat.

Unlike fusing smaller components like collars and cuffs, body fusing provides support across larger fabric areas. It helps the garment maintain its overall shape, structure and drape.

For tailored garments, a soft and flexible interlining is generally preferred for body fusing. This allows the garment to retain a natural feel while gaining the necessary support across the chest and front panels.

Common Applications in Garments

Interlining fabric is used in different parts of clothing depending on the structure and support required.

  • Collars: Helps maintain crisp collar points and prevents curling.
  • Cuffs: Provides firmness and helps cuffs retain their shape.
  • Jackets and suits: Supports lapels, chest areas and front panels through body fusing.
  • Waistbands: Helps prevent stretching and provides additional firmness.
  • Plackets: Supports button and buttonhole areas and helps maintain their shape.

By matching the interlining construction and weight to your garment requirements, you can achieve a more consistent finish.

What Should You Consider When Choosing Between Fabric Fusing and Fabric Bonding?

Fabric fusing and fabric bonding serve different purposes. The right choice depends on the material you are working with, the garment application and the finish you want to achieve.

Before selecting a method, consider the following factors.

Fabric Type and Garment Requirements

Start by understanding the type of fabric and its intended application.

For shirts, jackets, suits and other tailored garments, fabric fusing with suitable fusible interlining is commonly used to provide structure and support.

For waterproof outerwear, foam-backed materials and sealed seams, other bonding techniques, such as lamination or ultrasonic joining, may be more suitable.

You should also consider whether your main fabric is delicate, stretchy, heavily textured or sensitive to heat, as these characteristics can affect the joining process.

Required Structure and Flexibility

Think about how you want the finished garment or textile material to look and feel.

If you need to give a collar, cuff or jacket front a defined shape while retaining a soft feel, fabric fusing allows you to select an interlining according to the required level of support.

If your objective is to combine different materials to achieve specific properties, such as water resistance, insulation or sealed seams, a suitable fabric bonding method may be more appropriate.

Durability and Production Requirements

The final joining method should also match the expected use and production conditions.

Consider factors such as:

  • Expected wear and washing requirements.
  • Compatibility between the fabric and adhesive.
  • Production volume and available equipment.
  • Required temperature, pressure and application time.
  • Desired flexibility and long-term bond strength.

For fabric fusing, selecting compatible interlining and following the recommended fusing specifications are important. For other bonding techniques, you may need specialised lamination or ultrasonic equipment.

We recommend testing the selected materials and process on a small sample before moving to bulk production. This helps you identify possible issues such as bubbling, separation, stiffness or adhesive showing through the fabric.

Why Choose Double Ghoda for Your Interlining Fabric Requirements?

At Double Ghoda, we understand the important role interlining fabric plays in garment construction. The right supporting material can make a difference to the structure, stability and overall finish of your garments.

Whether you are exploring fusible interlining for collars and cuffs or looking into body fusing for jackets and suits, understanding your fabric requirements is the first step towards selecting a suitable material.

We believe that choosing interlining should involve more than simply considering its weight or appearance. You should also look at its construction, adhesive compatibility, flexibility and intended garment application.

Our focus on interlining fabrics helps us understand the different requirements involved in fabric fusing and garment manufacturing. We aim to help you understand these materials so you can make informed decisions for your textile and apparel requirements.

If you are exploring interlining options for your next garment project, connect with Double Ghoda to learn more about our interlining fabric offerings and find a suitable option for your application.
Link of related Articles

shweta-textile-designer
 
Shweta, a textile designer with a keen eye and deep knowledge of fabrics, translates her passion into unique designs. She loves to share her expertise and ignite a love for textiles in others. Dive into the world of fabrics with Shweta!

Categories
Fusible Interlining Interlining

How Adhesive Coating Affects Fusible Interlining Performance

Adhesive coating decides how well an interlining bonds to the outer fabric, and how that bond looks and lasts through pressing, wear and cleaning. A well-matched coating gives a firm, even bond and a clean surface. A mismatched one can lead to bubbling, stiffness or peeling. In fusible interlining, the coating works together with the base cloth, the outer fabric and your pressing process to shape the final result.

This guide covers what the coating does, how it influences bonding strength and garment appearance, which coating types you will meet, and how to choose with confidence. It is written for garment manufacturers, suit and blazer makers, apparel exporters and sourcing teams. Everything here is general textile guidance, apart from a short note on our own range in Section 6.

What Is Adhesive Coating in Fusible Interlining?

Adhesive coating is a layer of thermoplastic adhesive applied to one side of the base cloth. Under heat and pressure, it softens, grips the surface of the outer fabric and sets as it cools. That joins the two layers.

The base can be woven or non-woven. The coating sits on one face only, so the coated side must face the wrong side of the outer fabric.

Coatings are applied in different ways, such as dots, paste or powder. The adhesive type, the pattern and the amount of adhesive together decide how the material behaves when fused.

The trade uses many names for the same product. You may hear fusing cloth in Surat and across Gujarat, or interlining fabric in formal sourcing documents. Whatever the name, the coating is what makes the base cloth fusible. Good adhesive coating for interlining is a balance of adhesive type, coverage and compatibility.

Interlining Fabric

How Adhesive Coating Affects Bonding Strength and Fabric Durability

Coating shapes bonding strength through three things: how much adhesive is present, how evenly it is spread, and how well its melting behaviour suits your outer fabric and process.

  • Coverage: Even coverage generally gives a more uniform bond across the panel. Gaps can leave areas that lift later.
  • Adhesive type: Adhesives soften at different heat levels and respond differently to washing and dry cleaning. The coating should suit how the garment will be cared for.
  • Coating amount and dot size: Too little adhesive can bond weakly. Too much can push through the outer fabric or make the panel stiff.
  • Appearance: Adhesive that passes through the outer fabric is called strike-through. Adhesive that passes back through the interlining base is called strike-back. Both can spoil the surface or the hand-feel.

Durability depends on the whole system, not the coating alone. A bond that looks perfect off the press can still weaken after repeated cleaning if the adhesive and fabric are not compatible. No coating performs the same on every fabric, which is why we recommend testing finished samples through the same care process your garment will face.

Types of Adhesive Coatings Used in Fusible Interlining

Coatings differ by adhesive chemistry and by application method. The points below are general industry guidance. Behaviour varies by producer, so always confirm details against the supplier’s specification.

By adhesive type

AdhesiveGeneral characteristicsWhere it is commonly considered
Polyamide (PA)Often chosen for bond durability through cleaningStructured tailoring and formal wear
Polyester (PES)Often chosen where a softer hand is wantedLighter garments and smaller parts
Polyethylene (PE)Typically associated with washable garments; grades varyGarments that are laundered

By application method

  • Paste dot: Adhesive paste is printed as a pattern of dots, giving a consistent layout.
  • Double dot: Generally a two-layer dot, designed to support bonding while helping limit strike-through.
  • Powder or scatter: Adhesive powder is distributed and fixed to the base cloth. Suitability depends on the fabric and end use.

In our own range, the woven grades carry PA double-dot coating and the non-woven grades carry PES coating. Still, no single coating is best for every garment. The right choice depends on the interlining, the outer fabric and the application.

Fusible Interlining

How to Choose the Right Adhesive Coating for Different Garments

Choose by matching the coating, the interlining and the outer fabric to what the garment must do. Start with these questions:

  • Garment type and support: Structured garments need firm, lasting support. For full-front body fusing on suits, blazers and sherwanis, you generally look at a woven base with a coating chosen for durable bonding. Collars, cuffs and small parts usually need lighter support.
  • Outer-fabric construction: Open weaves, textured surfaces, delicate fabrics and stretch fabrics all bond differently. Finishes such as water repellents or silicone can reduce adhesion.
  • Heat sensitivity: Some outer fabrics tolerate less heat. Check this before you shortlist a coating.
  • Required hand-feel: A firmer coating and base give more body. A lighter combination keeps the fabric soft.
  • Care method: Dry-clean and wash-care garments can place different demands on the adhesive.

Here is a practical example. A heavily embroidered sherwani front and a lightweight blazer fabric both need fusing, but they ask very different things of the bond. The first needs strong, lasting support under a dense surface. The second needs a bond that stays invisible on a lighter cloth.

Always test before bulk production. Whether you call it fusing cloth or something else, follow this routine:

Record the results, then approve or adjust before bulk cutting.

Request samples of the interlining for suits or other garments you are making.

Fuse them on your actual production fabric, using your normal process and the supplier’s guidance.

Check the full panel and the edges for bond consistency and surface appearance after cooling.

Put the sample through the cleaning method your end use requires.

Common Fusible Interlining Problems Caused by Incorrect Adhesive Coating

Most fusing defects come from a mismatch between coating, fabric and process, rarely from one cause alone. The table lists possible causes to investigate. It is not a diagnosis.

ProblemPossible causesWhat to check
BubblingTrapped moisture or air, uneven pressure, coating not suited to the fabricFabric moisture, press uniformity, material compatibility
Delamination (peeling)Adhesive not matched to the outer fabric or care method, fabric finishesFabric finish, cleaning test results
Wrinkling or puckeringShrinkage difference between interlining and outer fabric, excess heatShrinkage of both materials, press conditions
Poor bondingLow adhesive coverage, finishes that repel adhesive, coated side facing wrong way, insufficient heat, time or pressureOrientation, fabric finish, supplier guidance on settings
Strike-throughToo much adhesive, very open weave, excess heat or pressureTrial on the real outer fabric
Stiff hand-feelHeavy coating or an over-firm baseCoating amount, base choice

Defects show up most on large panels, such as body fusing on a jacket front, so check those first. When something goes wrong, change one variable at a time and keep a record. Switching the interlining, the press settings and the fabric all at once makes the cause impossible to find.

Choosing Fusible Interlining from Double Ghoda

Double Ghoda, is a wholesale supplier and stockist.

Our fusible interlining range covers both woven and non-woven grades, with PA double-dot coating on the woven side and PES coating on the non-woven side. If you want to look closer at either, our woven interlining and non-woven interlining pages go grade by grade.

Before you order, get clear on four things:

  • The garment type and the support it needs
  • Your outer fabric and any finishes on it
  • How the garment will be cleaned
  • The grade and specification you are considering

We supply wholesale only, with a minimum order of 1,000 metres. If you are sourcing wholesale interlining fabric, confirming these points and testing a sample first saves time and avoids costly rework.

FAQs

What does adhesive coating do in fusible interlining?

It is the heat-activated adhesive layer on one side of the base cloth. It bonds the interlining to the outer fabric and influences how firm and even the bond is, and how the fused panel looks and feels.

How does adhesive coating affect bonding strength?

Bonding strength depends on adhesive type, coverage, coating amount and how well the coating suits your outer fabric and process. Even coverage and a well-matched adhesive generally support a more consistent bond. Confirm this with sample testing.

What causes bubbling or poor adhesion in fusible interlining?

Common causes include trapped moisture or air, uneven pressure, heat or time that does not suit the product, a coating that does not match the outer fabric, fabric finishes that repel adhesive, and shrinkage differences. Check them one at a time on a test sample.

Where can garment manufacturers explore fusible interlining options from Double Ghoda?

You can explore our woven and non-woven options on our official Double Ghoda product page. Share your garment type, outer fabric and quantity, and we will help you shortlist grades to sample.

Link of related Articles

shweta-textile-designer
 
Shweta, a textile designer with a keen eye and deep knowledge of fabrics, translates her passion into unique designs. She loves to share her expertise and ignite a love for textiles in others. Dive into the world of fabrics with Shweta!

Categories
Fusible Interlining Interlining

Fusing Cloth for Formalwear: Selecting the Right Support Layer

The right support layer for formalwear depends on the garment’s construction, the outer fabric, the area being reinforced, the silhouette you want and the level of structure required. A suit front, a lapel, a collar, a cuff and a waistband each need different support. That is why no single fusing cloth suits every formal garment.

This guide shows you how to match the support layer to the application. It covers fabric weight, woven and non-woven options, common selection mistakes and what to test before bulk production. 

What Is Fusing Cloth for Formalwear?

Fusing material is a base fabric coated with a heat-activated adhesive on one side. You press it onto the wrong side of the outer fabric. The adhesive bonds the two layers and gives that garment part shape, stability and body.

How does it support garment components?

Outer fabrics can be soft, loose or prone to stretching. Once bonded, the reinforcing layer helps the fabric hold its intended form. It also helps the fabric resist distortion during stitching, pressing and wear.

Where is it used in formalwear?

You will find reinforcing layers in several parts of a formal garment:

  • Suit and blazer fronts
  • Lapels and collars
  • Cuffs and plackets
  • Waistbands
  • Pocket areas and other small parts

Each part has a different job. A suit front needs a stable chest and shape. A cuff mainly needs a crisp, flat edge.

Interlining Fabric
Why one specification does not fit every application

Garment design and outer fabric both shape the choice. A fine wool, a textured blend and a heavily embroidered fabric all behave differently under heat and pressure. In the trade, the heavier support used across the full front of a jacket is often called body fusing. Smaller parts usually need something lighter. Treat the specification as a decision you make for each component.

Why the Right Support Layer Matters in Formalwear

The support layer sits inside the garment, but it affects how the garment looks from the outside. Material selection influences shape, finish and how the garment feels on the body.

  • Shape retention and silhouette

A formal garment is judged on its lines. Sharp lapels, a clean chest and a stable collar all depend on what sits behind the outer fabric. The right support helps the garment keep its intended silhouette through production and wear.

  • Structure, flexibility and drape

Every support layer balances three things: structure, flexibility and drape. More structure gives a firmer hand. Less structure keeps the fabric softer and more fluid. A tailored suit jacket and a lightweight formal garment sit at different points on that scale. Choose the balance that suits the design, not the heaviest option available.

  • Compatibility with the outer fabric

The outer fabric and the reinforcing layer must work together. If they do not, the bond can fail or the surface can change. A good match comes from testing the actual fabric with the actual material. Checking the specification sheet alone is not enough. Mismatched fabric weight and interlining fabric structure are common starting points for finishing trouble.

What can go wrong

Unsuitable selection may contribute to visible defects. These include:

  • Bubbling or rippling on the surface
  • Wrinkling around seams
  • Poor adhesion at edges
  • A stiff or board-like hand
  • Changes in the look of the outer fabric

These issues are general risks, not guaranteed outcomes. Careful selection and testing help you avoid them.

How to Choose Fusing Cloth Based on Fabric Weight and Structure

Start with the outer fabric. Then decide what each garment component needs to do. Work through the questions below in order.

Look at the outer fabric first

Weight, texture and construction all matter. A lightweight, fluid fabric can look stiff or heavy with too much support. A dense, structured fabric may need more support to hold its shape. Textured or loosely woven fabrics may also behave differently under heat, so test them early.

Define the support each component needs

Ask what the component must achieve:

  • Should the suit front hold a firm chest line, or follow the body softly?
  • Should a collar stand crisp or roll gently?
  • Does a waistband need stability without bulk?

Different answers lead to different materials, even within a single garment. This is also where body fusing decisions are made for the front panels.

  • Treat GSM as one factor

GSM measures fabric weight in grams per square metre. It is a useful starting point, but it is not a complete measure of suitability. Two materials with the same GSM can differ in construction, hand-feel and adhesive. They may also bond differently to the same outer fabric.

  • Does higher GSM always give better support?

No. A higher GSM does not automatically mean better support. The right weight depends on the outer fabric, the garment construction and the result you want. Too much weight can make a garment stiff or over-built. Too little can leave it under-supported. We do not suggest one GSM range for every garment, because no such range exists.

  • Balance flexibility, stiffness and finish

Decide what the finished garment should feel like. Think about how the fabric moves, how crisp the edge should look and how the surface should sit. Write these targets down before you compare materials. They give your team a shared standard to judge samples against.

  • Test samples before bulk production

Bonding compatibility is the main reason to test. Fuse a sample of your actual outer fabric with the candidate material. Then check the result for adhesion, surface changes and hand-feel. Follow the supplier’s instructions for the bonding process, and confirm the result on your own equipment.

Fusible Interlining

Woven vs Non-Woven Fusing Cloth for Formal Garments

Both categories have a place in formalwear. Neither is better in every situation. Suitability depends on the specific material, the garment design and the outer fabric.

How the two categories compare
FactorWovenNon-Woven
General constructionYarns interlaced in a woven structureFibres bonded together into a web
Typical application considerationsOften considered for larger, structured componentsOften considered for smaller or lighter components
Fabric compatibilityDepends on outer fabric and specific materialDepends on outer fabric and specific material
Support and finishCan offer firmer, more stable supportCan offer lighter, softer support
Bonding and testingFollow supplier instructions; test samplesFollow supplier instructions; test samples

This table gives general guidance only. Individual materials within each category vary, so the specific product matters more than the category label.

Choosing by application

For structured parts like jacket fronts, many manufacturers look at woven options first. For lighter parts or lighter garments, non-woven options are often considered. Many factories use both categories in the same garment, matched to each component. Your own testing should make the final call.

Bonding in general terms

Bonding uses heat, pressure and time to activate the adhesive. The right settings depend on the material and the outer fabric. We do not give universal temperature, pressure or time settings, because they vary by product and fabric. Follow your material supplier’s instructions, then test samples for:

  • Bubbling
  • Wrinkling
  • Poor adhesion or edge lifting
  • Changes in the appearance of the outer fabric

If a sample shows any of these, change the material or the process before moving ahead.

Common Fusing Cloth Selection Mistakes to Avoid

Most selection problems are avoidable. These are the ones we see most often.

1. Choosing by GSM alone

GSM is one factor. Weight tells you little about hand-feel, adhesive or compatibility. Use it to shortlist, not to decide.

2. Ignoring outer-fabric compatibility

A material that works on one outer fabric may fail on another. Always test on the fabric you will actually use.

3. Using one specification for every component

A suit front, a collar and a waistband have different needs. Matching each part to its own material usually gives a better result than applying one choice everywhere.

4. Skipping sample testing

Testing is quick compared with the cost of a failed production run. Fuse, cool and inspect samples before you commit to bulk.

5. Overlooking bonding conditions and finish

The bond and the finished look both depend on correct processing. Record your settings and the appearance you want, so results are repeatable.

6. Not checking batch consistency

A good first sample does not guarantee the same result in later lots. Check incoming batches against your approved sample.

7. Ordering in bulk before confirming the specification

Confirm the specification with samples first. Then plan your bulk quantity.

A simple evaluation process

Sourcing teams, manufacturers and exporters can follow a short checklist:

  1. Define the garment, component and desired finish.
  2. Shortlist materials based on the outer fabric.
  3. Test samples and record the results.
  4. Approve one specification per component.
  5. Check each batch against the approved sample.

A written process like this reduces avoidable rework. It also makes reordering simpler. When your team sources fusing cloth, this checklist helps keep every purchase consistent.

Choosing Fusing Cloth from Double Ghoda

Most formalwear problems start at the front panel, so begin there. Settle the front, then work outwards to the collar, cuffs and smaller parts.

That order matches how we organise our range at Double Ghoda. Our fusible interlining category separates woven grades, used for the main body of suits, blazers and sherwanis, from non-woven grades, used for collars, cuffs and plackets. Many factories buy from both sides for a single garment.

We work as a wholesale supplier and stockist under the B.C. Impex name. We do not manufacture what we supply, so our advice stays tied to your garment and not to a production line of our own.

Bring four details when you talk to us: the garment, the component, the outer fabric and the finish you want. With those, we can point you towards the right interlining fabric and weight. Not every grade suits every garment, and your outer fabric has the final say.

FAQs

What is fusing cloth used for in formalwear?

It adds shape, stability and structure to garment components such as suit fronts, lapels, collars, cuffs and waistbands. It is bonded to the outer fabric with heat and pressure. The right choice depends on the garment design and the outer fabric.

How do you choose the right GSM for formal garments?

Choose GSM based on the outer fabric, the garment component and the finish you want. Higher GSM does not always mean better support. Test samples on your actual fabric before bulk production.

What is the difference between woven and non-woven fusing cloth?

Woven material has interlaced yarns and is often considered for larger, structured parts. Non-woven material is made of bonded fibres and is often considered for lighter or smaller parts. Neither is better in every case. Suitability depends on the garment and the outer fabric.

Link of related Articles

shweta-textile-designer
 
Shweta, a textile designer with a keen eye and deep knowledge of fabrics, translates her passion into unique designs. She loves to share her expertise and ignite a love for textiles in others. Dive into the world of fabrics with Shweta!

Categories
Fusible Interlining Interlining

Fusing Cloth for Shirts vs Jackets: Understanding Application Requirements

The requirements for fusing cloth differ between shirts and jackets because each garment needs a different kind of support. Your shirts need light, flexible reinforcement in collars, cuffs and plackets. Your jackets and blazers need firmer support in the fronts, lapels and other structured areas.

The right choice depends on your garment construction, the area you are reinforcing, your outer fabric, the stiffness you want and the support your design needs. No single option suits every use, so we always suggest selecting by application, not by habit.

In this guide, we compare shirt and jacket requirements the way your production team would. We also cover GSM, bonding and sampling, so you can approve materials with confidence.

Understanding Fusing Cloth Requirements for Shirts and Jackets

Shirts and jackets need different support because they are built to behave differently. We expect a shirt to stay soft and move with the wearer. We expect a jacket to hold its shape and keep its lines.

Why garments use reinforcing materials

Your outer fabric often lacks the body to hold a shape on its own. A reinforcing layer adds structure, steadies edges and helps limit stretching during sewing and wear. When you choose the right interlining fabric, your finished garment looks and feels as you designed it.

How construction changes the support needed

Shirt components are small and lightweight. When you work on collars, cuffs and plackets, you need enough support to keep them crisp, but not so much that they feel stiff.

Jackets have larger, shaped areas. Your fronts, lapels and facings carry the silhouette, so they usually need firmer, more structured support.

Why outer fabric, design and finish matter

The same reinforcing material can behave differently on different outer fabrics. A fine cotton poplin, a heavy wool blend and a polyester suiting each respond in their own way. Your garment design and intended finish, whether crisp, soft or fluid, also guide the choice.

That is why one specification rarely suits every garment. In the next two sections, we look at your shirt and jacket applications in detail.

Interlining Fabric

Choosing the Right Fusing Cloth for Shirt Manufacturing

Shirt manufacturing calls for support that is light, stable and comfortable. The right level depends on your shirt style, your outer fabric and the finish you want.

Which areas of a shirt typically need reinforcement?

Here are the areas that most often need support in your shirts:

  • Collars: keep points sharp and the collar band flat.
  • Cuffs: help the cuff hold its shape through wear and washing.
  • Plackets and front openings: keep the button line straight and reduce puckering.

Balancing shape, flexibility and comfort

A formal dress shirt may need a crisper collar than a casual one. A soft-collar style may need only light stabilisation. Too little support lets edges curl or collapse. Too much makes the garment stiff and uncomfortable.

Your aim is shape retention that still feels natural against the skin.

Compatibility with cotton, blends and other outer fabrics

Cotton, polyester blends and other outer fabrics differ in weight, weave, finish and heat sensitivity. Fine fabrics can show adhesive marks or surface change if the reinforcing material is too heavy or poorly matched. If you work with stretch fabrics or special finishes, take extra care.

For this reason, we recommend matching fusible interlining for shirts to your outer fabric and the shirt part, not applying it by habit.

What to check before approving bulk production

  • Collar and cuff shape after fusing and after washing
  • Bond quality across the full part, including edges
  • Surface appearance, such as bubbling, ripples or shine
  • Hand-feel compared with your approved sample
  • Shrinkage behaviour of both layers

Run these checks on your actual outer fabric. A result on one fabric does not carry over to another.

Exploring Fusing Cloth Options for Jackets and Blazers

In jackets, blazers and formalwear, we look for support that builds the silhouette and keeps it through wear. It is a different job from shirt reinforcement.

Which areas of a jacket need structured support?

If you make suits or blazers, you will usually look at these areas:

  • Jacket fronts and chest area
  • Lapels and collars
  • Front edges and facings
  • Other shaped areas that must hold their form

In tailored garments, body fusing is a common way to support your front panel and keep the chest area smooth. Because it covers a large area, even a small mismatch shows quickly.

Lightweight jackets vs structured blazers

A lightweight, softer jacket needs support that lets the fabric drape. A tailored blazer or formal jacket usually needs firmer support to hold a defined shape. Neither approach is better in general. Each fits a different design, and your design decides.

How outer-fabric weight, drape and construction affect selection

Heavy suiting can carry more support. Fine or fluid fabrics need a softer touch, or they lose their drape. Fabric weave, stretch and finish also change how the bond looks and feels.

What should manufacturers consider when selecting material for a blazer?

  • The blazer style and how structured it should look
  • Outer-fabric weight, drape and composition
  • The areas being reinforced
  • The stiffness and finish you want
  • How the material behaves under your fusing conditions

We would not say any single material suits every jacket. Test compatibility on your actual fabric before you scale up production.

Fusible Interlining

Comparing GSM, Bonding and Fabric Compatibility for Different Garments

In general, shirts use lighter, more flexible reinforcement, while jackets use firmer, more structured constructions. The table below summarises the main selection factors we suggest you compare. Treat it as general guidance, and confirm each point through your own testing.

FactorShirtsJackets and blazers
Typical application areasCollars, cuffs, plackets, front openingsFronts, lapels, collars, facings, structured areas
Required level of supportLight to moderate, with flexibilityModerate to firm, to hold the silhouette
GSM considerationsGenerally lighter weights, matched to the partGenerally heavier weights, matched to the design
Outer-fabric compatibilityCotton, blends and fine shirting fabricsSuiting, wool blends and heavier fabrics
Bonding requirementsEven, clean bond without surface marksStrong, uniform bond across large panels
Desired garment finishCrisp but comfortableShaped, smooth and stable
Pre-production testingWash test, bond check, appearance checkBond check, drape check, appearance check

Does a higher GSM always provide better support?

No. A higher GSM adds weight and usually stiffness, but it does not guarantee a better result. A heavy material on a light outer fabric can feel rigid and may show through the surface. The right weight and construction depend on your garment, your outer fabric and the finish you need.

Understanding bonding in general terms

Bonding happens when the adhesive on the reinforcing material melts under heat and pressure, then sets as it cools. Suitable fusing conditions depend on the material and the outer fabric. If you work with heat-sensitive fabrics, take particular care.

Body fusing on a jacket front shows poor adhesion quickly because the panels are large. We suggest you inspect samples for bubbling, wrinkling, poor adhesion and changes in fabric appearance.

We do not give universal temperature, pressure or time figures here, because they vary by material and fabric. Follow the material supplier’s instructions and your own production requirements when you test.

Finding the Right Fusing Cloth for Your Garment Production Needs

A technical comparison only helps once it turns into a clear purchasing decision. We suggest these steps to move you from specification to bulk order.

  1. Identify the garment and application area. A shirt collar and a jacket front are different jobs.
  2. Confirm the outer fabric and desired finish. Note composition, weight and drape.
  3. Define the support you need. Decide how crisp, soft or structured the area should be.
  4. Review the specification. Check GSM, construction, coating, width and roll requirements where relevant.
  5. Test samples. Approve nothing for bulk production before testing on your actual fabric.
  6. Check consistency. Compare batches for weight, hand-feel and bonding behaviour.
  7. Confirm quantity and stock needs. Agree order quantity, stock requirements and procurement timelines with your supplier.

A clear specification sheet makes every later step easier. When you write down the garment, area, fabric and finish, you also give your supplier what they need to guide you well.

These checks help you, whether you are a garment manufacturer, sourcing team or exporter, decide on facts instead of assumptions. For your export orders, consistent quality across batches matters as much as the first approved sample.

When you compare fusing cloth options, ask each supplier for the same information in the same format. It keeps the comparison fair and speeds up approval.

Explore Fusible Interlining Fabrics at Double Ghoda

We work with garment manufacturers, suit makers, sourcing teams and wholesale buyers. We are not a manufacturer.

Picking the right interlining for each garment application saves you rework later. On our official page, we list woven and non-woven grades across a 30 to 150 GSM range. Woven grades are listed for structured garments such as suits, blazers and sherwanis. Non-woven grades are listed for smaller parts such as collars, cuffs and plackets.

Not every grade suits every garment. We ask you to check your application, outer fabric and specification before you buy. Our page also includes a GSM guide and a woven vs non-woven comparison to help you review options.

We suggest you test samples first, then plan your bulk order around what works on your fabric. When you are ready, explore our fusible interlining range and review the product information.

m our product guide, not universal rules. Your outer fabric and intended finish still decide the final choice. Tell us what you are making and what outer fabric you are using, and we will help you shortlist suitable grades. You can view the full range on our official product page.

FAQs

What is the difference between fusing cloth for shirts and jackets?

Shirts generally need light, flexible support in collars, cuffs and plackets. Jackets generally need firmer support in fronts, lapels and other structured areas. In our view, the right choice depends on your garment construction, outer fabric, desired finish and the support you need.

How do you choose the right GSM for garment fusing?

We suggest you start with the garment area and your outer fabric, then decide how much support and stiffness your design needs. A higher GSM is not automatically better. Confirm your choice by testing samples and following your material supplier’s guidance.

Why should manufacturers test bonding compatibility before bulk production?

Testing shows you how the material behaves on your actual outer fabric. It reveals issues such as bubbling, wrinkling, poor adhesion or changes in fabric appearance before they affect your full production run.

Where can garment manufacturers explore fusible interlining options from Double Ghoda?

You can review our woven and non-woven grades, GSM guide and product details on our official interlining category page.

Link of related Articles

shweta-textile-designer
 
Shweta, a textile designer with a keen eye and deep knowledge of fabrics, translates her passion into unique designs. She loves to share her expertise and ignite a love for textiles in others. Dive into the world of fabrics with Shweta!

Categories
Fusible Interlining Interlining

Interlining Fabric for Structured vs Soft Garments: What Changes?

Structured garments need interlining that supports shape and stability. Soft garments need support that does not strip away drape, flexibility or hand feel. That is the core change. The right choice depends on garment structure, outer fabric and the finish you want, not on GSM alone.

If you are selecting interlining fabric for a new style, this guide shows how your requirements shift between the two garment types and how to decide with confidence. We wrote it for garment, suit and blazer manufacturers, exporters, sourcing teams and wholesale buyers.

What Is the Role of Interlining in Structured and Soft Garments?

Interlining is a hidden support layer that gives a garment part its shape, stability and control. How much support you need depends on how the garment is designed to look and move.

It sits between the outer fabric and the lining. Fusible grades carry a heat-activated adhesive on one side, so they bond to the outer fabric under heat and pressure. Many buyers simply call this product fusing cloth.

Requirements differ because a structured garment must hold a defined form, while a soft garment must keep its natural fall. With too little support, a jacket front can lose its shape. With too much, a flowing garment turns stiff.

Seven factors drive the choice:

Garment application: Where the interlining sits, such as the front body, collar, cuff, placket, waistband or pocket.

Garment structure: Is the design tailored, semi-structured or relaxed?

Outer fabric: Weight, weave, stretch and surface all change how interlining behaves.

Desired shape: Crisp and defined, or gentle and fluid.

Support: How much stability each panel needs.

Drape: How the cloth falls and moves.

Hand feel: How the finished garment feels to the touch.

Interlining Fabric

Interlining for Structured Garments: What Changes?

For structured garments, choose interlining that adds stability and defined shape while keeping the garment wearable. Think suits, blazers, jackets, coats and many uniforms, where the silhouette must hold through wear and cleaning.

What should you check for structured garments?

  • Required structure: A sharp chest and lapel need more support than a lightly tailored jacket.
  • Outer fabric: Heavier or textured cloth may need a different base than a fine, smooth one.
  • Garment component: Front body, chest, collar, lapel and cuff rarely need the same support level.
  • Interlining weight: Heavier weights generally add firmness, but weight is only one input.
  • Construction: Woven and non-woven bases behave differently under stress.
  • Coating: Adhesive type and dot pattern affect bond strength and fusing behaviour.
  • Bonding requirements: Consider cleaning method, wear cycles and bond durability.

General industry guidance: fusible interlining for structured garments is often woven, because a woven base generally offers more stability and shape retention. Lighter non-woven grades more often go into smaller parts. Treat this as a starting point, then confirm it with a test on your own outer fabric.

Do not assume one weight suits every suit or every coat. A heavily structured design in a soft cloth can need different support than a lighter design in a crisp cloth.

Interlining for Soft Garments: What Changes?

For soft garments, choose the lightest support that still does the job. The goal is to stabilise key areas while protecting the garment’s drape, flexibility and hand feel.

Soft garments include relaxed shirts, flowing tops, unstructured jackets, light formal wear and styles in fine or sheer cloth. They still need support in places such as plackets, necklines, waistbands and pockets.

Interlining fabric for soft garments usually comes down to these points:

  • Support requirements: Decide what must be held in place, such as an edge, opening or seam, rather than automatically fusing everything.
  • Outer fabric: Fine, lightweight or sheer cloth is easy to overpower with a stiff layer.
  • Garment construction: Full-panel fusing and part-only fusing give very different results.
  • Flexibility: The interlining should move with the cloth, not against it.
  • Drape: A stiff layer can interrupt the way a garment falls.
  • Hand feel: Judge the fused sample by hand, not by the spec sheet alone.

No single interlining type or GSM suits every soft garment. A light woven grade may work on one cloth, and a non-woven grade on another. Make the final call with a fused sample on your actual fabric.

Fusible Interlining

Structured vs Soft Garments: How Should Interlining Requirements Differ?

Structured garments generally need firmer, more stable support. Soft garments generally need lighter, more flexible support. The table shows the usual differences.

FactorStructured garmentsSoft garments
Garment structureDefined, tailored shapeRelaxed or fluid shape
Required supportHigher, often across larger panelsLower, often targeted to specific areas
Outer fabricOften firmer or heavier cloth, though not alwaysOften lighter or finer cloth, though not always
DrapeControlled and heldNatural and free-falling
Hand feelFirmer and crisperSofter and more pliable
Interlining constructionFrequently woven for stabilityLight woven or non-woven, depending on the cloth
WeightOften heavierOften lighter
ApplicationFront body, chest, lapel, collarPlackets, waistbands, necklines, pockets

The same garment category can need different interlining depending on design, outer fabric and finish. A tailored blazer in heavy wool and an unstructured blazer in linen are both blazers, yet they will not want the same support.

Application matters too. Using body fusing across the full front creates a different result than fusing only the edges. Decide the finish first, then pick the interlining that delivers it.

What Should Garment Manufacturers Consider Before Choosing Interlining?

Choose in sequence, starting with the garment and ending with production. This order keeps GSM in its proper place as one input, not the starting point.

Production requirements: Confirm press conditions, line speed, cleaning method and quality checks.

Garment structure: Define how structured the design is.

Outer fabric: Note weight, weave, stretch and finish.

Required support: Decide how much stability each garment component needs.

Drape and hand feel: Set how the finished garment should fall and feel.

Interlining construction: Choose woven or non-woven for the job.

GSM and weight: Shortlist weights that suit steps 1 to 5.

Coating: Check the adhesive type and pattern.

Why should GSM not be judged alone?

GSM tells you weight per square metre. It does not tell you the base construction, the coating or how the product feels once fused. Two products at the same GSM can behave differently, so compare them on a fused sample, not on weight alone.

Buyer recommendation: Before a bulk order, run a small fusing test on your actual outer fabric. Check bond strength, surface appearance, hand feel and how the fused part behaves after pressing and cleaning.

Ask your supplier for the recommended press conditions for each fusing cloth grade, and follow them in production. Wholesale buyers should also request clear specifications, such as construction, coating, width and roll format, so offers can be compared fairly.

Interlining Fabric Options From Double Ghoda

We are B.C. Impex, an import and wholesale trading business, and we supply woven and non-woven fusible interlining.

OptionGSM rangeCoatingTypical use listed on our site
Woven30–150 GSMPA double-dotGarment body in suits, blazers and sherwanis
Non-woven30–82 GSMPESCollars, cuffs, plackets and small parts

For structured garments, our woven range is where most buyers start. Our product guide lists 80–130 GSM woven for structured suits, with 120–130 GSM for premium suits that need a firmer chest. For blazers, it lists 80–120 GSM woven, with 100–120 GSM for heavily structured or premium styles. For heavier ethnic formal wear such as bandgala, Nehru jackets and achkans, it lists 100–150 GSM woven.

Body fusing refers to the heavier woven grades, 100–150 GSM, applied across the full front of a suit or sherwani. Our 140 GSM grade, known in the trade as 111 quality, is listed for sherwani full-front construction.

For softer and lighter applications, our guide lists 30–60 GSM woven or non-woven for ladies’ ethnic wear, light formal wear, waistbands and pockets. It lists 30–40 GSM woven as ultralight reinforcement for sheer fabrics and delicate women’s wear. Our non-woven grades are described as having good elasticity, so they move with the garment part.

Many factories use both: woven for the garment body and non-woven for collar and cuff details. Our woven range uses PA double-dot coating, and both ranges are listed as OEKO-TEX® Standard 100 certified.

Treat these figures as reference ranges from our product guide, not universal rules. Your outer fabric and intended finish still decide the final choice. Tell us what you are making and what outer fabric you are using, and we will help you shortlist suitable grades. You can view the full range on our official product page.

FAQs

What is the difference between interlining for structured and soft garments?

Structured garments need interlining that supports shape and stability. Soft garments need lighter, more flexible support that protects drape and hand feel. The right choice depends on garment design, outer fabric and finish.

Is higher GSM interlining always better for structured garments?

No. Higher GSM adds weight, but construction, coating and outer fabric also decide the result. Too much weight can make a garment over-stiff, so test a fused sample before you commit.

Can the same interlining be used for structured and soft garments?

Sometimes, but not by default. The same grade can suit one structured design and one soft design if the outer fabric and finish allow it. Always verify with a fusing test.

How does outer fabric affect interlining selection?

Outer fabric weight, weave, stretch and surface change how interlining bonds and how the garment feels afterwards. A fine or sheer cloth usually calls for lighter support than a heavy, firm cloth.

Link of related Articles

shweta-textile-designer
 
Shweta, a textile designer with a keen eye and deep knowledge of fabrics, translates her passion into unique designs. She loves to share her expertise and ignite a love for textiles in others. Dive into the world of fabrics with Shweta!

Categories
Fusible Interlining Interlining

Fusing Cloth for Apparel Manufacturing: Key Specifications to Compare

When you compare fusing cloth for apparel manufacturing, look beyond GSM. The specifications that matter are compatibility with your garment fabric, the structure your garment needs, your fusing process, bonding, finish, and roll specifications. No single GSM, construction, or coating suits every garment.

In this guide, we show you what to compare, why each specification matters, and what to confirm before a bulk order. Figures from our own product page are marked “we state.” Everything else is general industry guidance.

How to Match Fusing Cloth With Your Garment Fabric

Choose your fusing material for the fabric it will support, not as a standalone item. Your outer fabric’s weight, construction, and finish decide how much support the interlining should add.

What to compareWhy it matters to you
Fabric weightA light fabric can feel stiff under a heavy interlining. A heavy fabric can look under-supported with a light one.
Fabric constructionWoven, knit, and textured fabrics respond differently to heat, pressure, and adhesive.
Garment structureA tailored jacket front needs more support than a casual shirt panel.
Required supportDecide whether the part needs shape, stability, or light reinforcement.
Garment sectionCollars, cuffs, plackets, and front panels do different jobs.
Desired finishA crisp, soft, or fluid result points to different choices.

Think about a formal jacket and a shirt. Your jacket front is large and must hold chest and lapel shape, so body fusing in a woven construction is a common choice. Your shirt collar is smaller and needs crispness without a board-like feel, so a lighter grade is usually enough. One factory, two different interlining decisions.

A poor match shows up in your finished garment as stiffness, weak shape, or an uneven surface. Fabrics vary too much for any chart to pair every fabric with one interlining. Use charts as a starting point, and confirm with a sample.

Interlining Fabric

Which Fusing Cloth GSM Works for Apparel Manufacturing?

No single GSM works for every apparel application. GSM (grams per square metre) indicates the weight of the interlining and, broadly, the level of support. Read it alongside your fabric weight, garment type, construction, and intended use.

These GSM ranges by garment part:

Garment partGSM we stateType we state
Sheer or delicate reinforcement30–40Woven
Collars, cuffs, plackets40–60Woven
Light jacket parts, waistbands, pockets55–70Woven
Lightweight garments30–60Woven or non-woven
Blazers80–120Woven
Structured suits80–130Woven
Heavy ethnic formal wear100–150Woven

Our woven grades run 30–150 GSM and our non-woven grades run 30–82 GSM.

These ranges overlap on purpose. Your garment may use different weights in different sections: a heavier grade across the front, a lighter one on the collar, and something lighter again at the waistband. Using one GSM throughout can leave some parts over-stiff and others under-supported.

How do woven and non-woven differ? Our woven interlining has yarns interlaced in both directions, which makes it stronger and better at holding shape. Non-woven is made of bonded fibres. It is lighter, more economical, and suited to smaller parts where you don’t need full structural support. Neither is better in general. Your choice depends on the garment part.

How Fusing Conditions Affect Fusible Interlining Bonding

Fusing conditions decide whether the adhesive activates properly and bonds evenly. Fusible interlining is a base fabric, woven or non-woven, coated on one side with thermoplastic adhesive. Under heat and pressure, the adhesive melts and bonds to your fashion fabric.

In general industry practice, four variables work together:

  • Temperature: the adhesive must reach its activation point. Too little can leave a weak bond. Too much can damage heat-sensitive fabric.
  • Pressure: it brings the adhesive into contact with the fabric surface.
  • Dwell time: it gives heat time to pass through the fabric and activate the adhesive.
  • Fabric compatibility: thickness, fibre content, and finish affect how heat and pressure reach the adhesive.

Garment-technology references treat temperature, pressure, and time as the core fusing parameters. A cycle that is too short can leave the bond incomplete, while one that runs too long can push adhesive through to the face of the fabric, a defect known as strike-through (Online Clothing Study). 

Uneven settings across a panel or between batches lead to inconsistent bonding.

For flatbed pressing, we state 125–145°C for woven grades with PA coating, and up to 120°C for non-woven grades with PES coating. We state 18–25 seconds at 1.5–2.5 kg/cm². We also advise placing the coated side, which feels slightly rougher, against the wrong side of your fashion fabric.

These are our stated figures, not a universal rule. Your fabric may need different settings, so confirm the fusing requirements for each interlining and fabric pairing before you start production.

Fusible Interlining

What to Check for Fusing Cloth Performance and Garment Finish

Check bonding, appearance, hand feel, garment structure, compatibility with your outer fabric, and consistency across the production run.

  • Bonding: we state that you should look for no bubbles, no edge lifting, and consistent adhesion across the full panel, after the panel has cooled completely.
  • Appearance: look for surface ripples or visible marks on the face of your fabric. This is general guidance.
  • Hand feel: the fused section should feel right for the garment. A collar and a jacket front need different results.
  • Garment structure: does the part hold its shape in handling and on the body?
  • Compatibility: check that your outer fabric shows no unwanted change after fusing.
  • Consistency: compare early and late pieces in a run, and one batch against the next.

A sample or production trial helps most when you use a new fabric, a new supplier, or a new garment construction. A small trial on your own fabric, with your own press settings, is a practical way to vet fusing cloth before you commit to bulk volume. It reveals problems that a specification sheet cannot. Record the settings you used so you can repeat the result.

Which Roll Specifications Matter for Bulk Apparel Production?

Width, roll length, GSM, construction, coating, and total quantity. Interlining fabric is bought by the roll, so these physical specifications affect your cutting layouts, roll changes, and how far the material goes.

  • Width: it should suit your pattern pieces and cutting layout. Check it against the largest panel you cut.
  • Roll length: it affects how often your cutting tables need a roll change and how you plan quantities.
  • GSM and construction: confirm both match your approved sample. A matching GSM alone doesn’t guarantee a matching woven or non-woven structure.
  • Coating: confirm the adhesive type, because it ties to the fusing conditions on your production line.
  • Quantity: calculate the metres you need from your cutting plan and garment volume.

Our woven grades come in 50 m rolls at 150 cm width, and our non-woven grades in 90 m rolls at 100 cm width.

Before you order, compare the stated roll specifications against your cutting plan, approved sample, and production schedule. If anything on a specification sheet is unclear, ask us or any supplier directly.

Fusing Cloth and Fusible Interlining From Double Ghoda

We supply both woven and non-woven fusible interlining from 30 to 150 GSM. We state that both types are dry-clean safe and OEKO-TEX® Standard 100 certified.

We use body fusing as the trade term for our heavy woven grades of 100–150 GSM used in full-front construction. Our 140 GSM “111 quality” is the flagship grade we state for sherwani fusing.

SpecificationWoven (as we state)Non-woven (as we state)
ConstructionWoven polyester yarnsBonded polyester fibres
CoatingPA double-dotPES
GSM range30–15030–82
Roll length50 m90 m
Width150 cm100 cm
ColoursWhite, black, grey/charcoalWhite, black
Fusing temperature125–145°CUp to 120°C
Primary useSuits, blazers, sherwanis (full front)Collars, cuffs, plackets, pockets

You can use these specifications as a decision path:

your garment fabric → required structure → construction → GSM → coating → roll specification

For example, if you make a premium suit in a mid-to-heavy fabric, the front points to woven construction. That narrows your GSM to the woven range we state for suits, which in turn sets the coating (PA) and the roll format (50 m, 150 cm). A shirt placket moves down the same path to a lighter grade and the 90 m, 100 cm format. In both cases, confirm your final choice with a sample on your own fabric.

The figures here are as stated on our page when this was written. Please verify current specifications with us before you order.

FAQs

What is fusing material used for in apparel manufacturing?
It adds structure, shape, and stability to garment parts such as collars, cuffs, plackets, and jacket fronts. Heat and pressure bond a coated base fabric to your outer fabric.

How do you choose the right GSM?
Match it to your fabric weight, garment type, and the support each section needs. There is no universal GSM. Lighter grades suit small parts, and heavier grades suit structured garment fronts. Confirm with a sample.

What is the difference between woven and non-woven fusible grades?
Woven grades use interlaced yarns and are stronger, which suits garment bodies. Non-woven grades use bonded fibres and are lighter, which suits smaller parts. We state that our woven grades run 30–150 GSM and our non-woven grades 30–82 GSM.

Why do fusing conditions matter for garment production?
Temperature, pressure, and dwell time control adhesive activation. Incorrect or uneven settings can cause weak or inconsistent bonding. Confirm the conditions on your own fabric before production.

What roll specifications should you check before ordering?
Width, roll length, GSM, construction, coating, and total quantity. Check each against your cutting layout and approved sample.

What do we supply?
We supply woven and non-woven fusible grades from 30 to 150 GSM. We state PA double-dot coating on woven and PES coating on non-woven.

Before you order, confirm six things: your garment fabric and section, the construction, the GSM, the coating, your fusing conditions, and the roll width and length. Then test the match on a sample. Settling these before a bulk purchase of interlining fabric keeps your decision tied to your production needs rather than to a single number.

Link of related Articles

shweta-textile-designer
 
Shweta, a textile designer with a keen eye and deep knowledge of fabrics, translates her passion into unique designs. She loves to share her expertise and ignite a love for textiles in others. Dive into the world of fabrics with Shweta!

Categories
Fusible Interlining Interlining

PA vs PES Coating in Fusible Interlining: Which to Order

If you’re comparing PA and PES coating before placing a bulk order, here’s the short answer: there isn’t a single “better” coating, the right one depends on the interlining construction, the garment part, the structure you need, the GSM, and the application. PA coating is used with woven fusible interlining and is built for structured garment bodies. PES coating is used with non-woven interlining and is built for lighter, smaller garment parts. Your job as a buyer isn’t to pick a “winner”, it’s to match the coating to what you’re actually constructing.

This guide breaks that decision down so your sourcing team can order the right interlining fabric the first time, without guesswork.

What Are PA and PES Coatings in Fusible Interlining?

Fusible interlining is a base fabric — woven or non-woven — coated on one side with a thermoplastic adhesive. When you press it against your fashion fabric with heat and pressure, that adhesive melts and bonds the two layers together permanently. This is what gives a collar its crispness or a suit front its shape.

PA stands for polyamide, and PES stands for polyester — both are types of adhesive used to coat interlining. The coating isn’t chosen at random; it’s tied directly to how the interlining itself is built.

Woven fusible interlining, made from interlaced polyester yarns, is typically finished with a PA double-dot coating. In this pattern, the adhesive is applied as two staggered rows of dots, which increases coverage and helps the coating bond more completely across the panel. Non-woven fusible interlining, made from bonded fibres rather than a woven structure, is typically finished with a PES coating instead.

So before you ask “PA or PES,” it helps to ask “woven or non-woven” — the coating usually follows the construction, not the other way around.

Interlining Fabric

PA vs PES Coating: What Is the Difference?

At a glance, PA and PES coatings differ less in the chemistry a buyer needs to memorise and more in what they’re paired with and where they end up in a garment.

FactorPA CoatingPES Coating
Typical constructionWoven fusible interliningNon-woven fusible interlining
Application patternDouble-dotCoated finish
Garment roleStructured body panelsSmaller, lighter parts
General strengthHigher tensile and tear strengthModerate — sufficient for its use case
Typical GSM rangeRuns into the heavier gradesStays in the lighter grades

Woven grades with PA coating are generally positioned as stronger and better suited to structured garment bodies, while non-woven grades with PES coating are positioned as lighter and better suited to smaller garment parts. Neither is a universal upgrade over the other — a heavier, stronger construction isn’t useful on a collar that needs to stay soft and move with the fabric, and a lighter non-woven construction won’t hold a suit front’s shape.

This is the core purchasing logic: coating type is a signal of what the interlining is designed to do, not a standalone quality marker.

When Should You Order PA-Coated Fusible Interlining?

Order PA-coated woven interlining when the garment needs real structure — a panel that holds its shape through wear, movement and repeated cleaning.

This is the standard choice for:

  • Suits
  • Blazers
  • Sherwanis
  • Full-front body fusing on structured formal wear

The logic here is straightforward: woven construction → PA coating → structural garment applications. A suit front or sherwani body needs to resist distortion and keep a clean silhouette, and the woven base with its PA double-dot coating is built for that job.

That said, PA-coated interlining isn’t the automatic answer for every part of every garment. A full sherwani body needs it; the collar sitting above it may not. Ordering PA-coated interlining for a component that only needs light support usually means paying for structure you don’t need and ending up with a stiffer hand-feel than the part calls for.

When Is PES-Coated Interlining the Better Fit?

PES-coated non-woven interlining is the better fit when a garment part needs support without heavy structure — where you want the fabric to keep moving naturally rather than hold a rigid shape.

Common applications include:

  • Collars
  • Cuffs
  • Plackets
  • Pockets
  • Other smaller garment parts

The question to ask isn’t “is PES weaker than PA” — it’s “how much structure does this specific part actually need.” A collar that’s over-stiffened looks and feels wrong on the finished garment, even if the bond itself is sound. PES-coated non-woven interlining is generally lighter, which suits parts where flexibility and a soft hand matter as much as support.

Choosing PES coating here isn’t a compromise — it’s the correct call for the job, in the same way PA is correct for a body panel. The two coatings solve different problems, and buyers who treat this as PA-good, PES-lesser tend to over-spec their smaller components.

How Do GSM, Garment Type and Application Affect Your Choice?

Coating type is only one part of the order. GSM — grams per square metre — is what actually determines how much structure the interlining fabric delivers, and it should be considered alongside, not instead of, your coating decision.

As a general reference, woven grades span a GSM range from roughly 30 to 150, and non-woven grades from roughly 30 to 82. A higher GSM generally means a heavier, firmer interlining; a lower GSM means a lighter one. Two woven fabrics can both carry a PA coating and still behave very differently on the sewing floor purely because of GSM.

Practically, this means your order should factor in:

  • Garment type — a lightweight kurta and a heavy bandgala jacket don’t need the same GSM, even in the same construction category.
  • Garment section — the body, collar, cuffs and pockets of a single garment can each call for a different interlining fabric.
  • Fabric weight — heavier outer fabrics usually need a heavier interlining to fuse well and hold shape.
  • Desired hand-feel — how stiff or soft the finished part should feel to the wearer.
  • Production requirements — what your fusing setup and workflow are already calibrated for.

This is also why the same garment often needs two orders, not one. A structured jacket might need woven, PA-coated interlining at a heavier GSM for the body, and non-woven, PES-coated interlining at a lighter GSM for the collar and cuffs. Treating “PA vs PES” as a single, garment-wide decision is where most sourcing mismatches happen — the decision is really made part by part.

Before placing a bulk order, it helps to check: the construction (woven or non-woven), the GSM range appropriate to the garment part, and how the interlining will actually be pressed and finished in your process. Getting these three aligned matters more than picking a coating in isolation.

Which Fusible Interlining Should You Order From Double Ghoda?

We supply both woven and non-woven fusible interlining, so you can source your structured panels and your smaller garment parts from a single order rather than two separate suppliers.

Here’s how our range maps to the decision above:

  • Our woven fusible interlining uses PA double-dot coating and is positioned for structured garment bodies — suits, blazers and sherwanis where the panel needs to hold its shape.
  • Our non-woven fusible interlining uses PES coating and is positioned for collars, cuffs, plackets and other smaller garment parts that need lighter support.

If you’re placing an order and aren’t sure which to choose, start with the part of the garment you’re fusing, not the coating name. Ask yourself whether that part needs to hold a structured shape (woven, PA-coated) or stay light and flexible (non-woven, PES-coated), then narrow down the GSM based on your fabric weight and garment type. If a single style needs both — a formal jacket with a structured body and a soft collar, for instance — you can order both constructions together and match each to the relevant panel.

Whichever you need, we’re happy to talk through the specifics of your garment before you place a bulk order, so the interlining you receive actually matches the construction you’re building.

FAQs

What is PA coating in fusible interlining?
PA stands for polyamide, the adhesive used to coat woven fusible interlining. It’s typically applied in a double-dot pattern, which is associated with woven grades built for structured garment applications.

What is PES coating in fusible interlining?
PES stands for polyester, the adhesive used to coat non-woven fusible interlining. It’s associated with lighter grades used on smaller garment parts such as collars and cuffs.

What is the difference between PA and PES coating?
The main difference is what they’re paired with and where they’re used: PA coating goes with woven interlining for structured body panels, while PES coating goes with non-woven interlining for lighter, smaller parts. Neither is universally better — the right choice depends on the garment part and required structure.

Is PA coating always used on woven interlining?
Woven fusible interlining is generally finished with PA double-dot coating, since the combination is built to deliver stronger, more structured support.

Is PES coating always used on non-woven interlining?
Non-woven fusible interlining is generally finished with PES coating, matching its lighter, more flexible construction.

Which coating should I order for suits, sherwanis, collars or cuffs?
For suits, blazers and sherwani bodies, PA-coated woven interlining is the standard choice. For collars, cuffs, plackets and other smaller parts, PES-coated non-woven interlining is generally the better fit. Many garments need both, ordered for their respective parts.

Link of related Articles

shweta-textile-designer
 
Shweta, a textile designer with a keen eye and deep knowledge of fabrics, translates her passion into unique designs. She loves to share her expertise and ignite a love for textiles in others. Dive into the world of fabrics with Shweta!

Categories
Fusible Interlining Interlining

Does Fusible Interlining Shrink? How to Pre-Test a Batch

Yes, fusible interlining can shrink or change dimensions. Heat and pressure during fusing, and later washing or dry cleaning, can cause a small amount of dimensional change in the base fabric, the adhesive coating, or both. In most cases the change is minor and expected. The risk comes when it doesn’t match the shrinkage of your shell fabric, that’s what causes puckering, bubbling, or a panel that no longer lies flat.

This is why we always recommend you don’t take a roll straight into bulk cutting. Test a sample of the batch first, fuse it, cool it, and put it through the same washing or dry-cleaning process your finished garment will face, before you commit the full order to production.

Here’s why dimensional change happens, what it does to a garment when it’s out of step with the shell fabric, and how you can run a practical pre-test on any batch before full production starts.

Why Does Fusible Interlining Shrink?

Dimensional change happens because heat, moisture, and mechanical tension act on the fibers, the bonding or weave structure, and the adhesive coating, and none of those materials respond identically.

A few factors drive it:

  • Heat-setting during fusing. Your press applies heat and pressure to melt the adhesive and bond it to the shell fabric. That same heat can relax residual tension left in the interlining fabric from manufacturing, letting fibers or yarns pull back slightly.
  • Construction type. A woven base holds its yarns in a fixed grid, so it tends to move less than a bonded-fiber, non-woven structure. Non-woven grades can respond a little differently to heat, and their behavior can vary more between production lots.
  • Moisture exposure. Washing or dry cleaning introduces moisture and mechanical agitation, which can cause a second, smaller round of dimensional change after the garment leaves your factory.
  • Coating and finishing. The adhesive coating and any pre-treatment applied to the base cloth can affect how the material relaxes under heat, independent of the fiber itself.
  • Roll-to-roll and lot-to-lot variation. Even within the same specification, raw material and finishing can vary slightly between production runs. That’s one reason a batch that performed well before still deserves its own check.

None of this means the material is defective. It means dimensional behavior is a real, measurable property that varies by construction and by batch, and that’s exactly what a pre-test is designed to catch before it reaches your finished garment.

Interlining Fabric

What Happens When Interlining Shrinks Differently From the Fabric?

The problem isn’t shrinkage on its own, it’s a mismatch between how much the interlining moves and how much your shell fabric moves. When the two are out of step, the bonded panel can’t stay flat.

Typical signs on a finished panel include:

Bubbling or puckering across the fused area, especially visible on structured suit fronts and lapels under good light

Edge lifting or delamination at panel edges, where uneven tension pulls at the bond line

Distorted seams where a fused panel no longer matches the dimensions of the panel it’s sewn to

A stiffer or looser hand-feel than intended, if the material pulled tighter or looser than the fabric around it

Problems that only appear after the first wash or dry clean, once the garment has been through the cleaning cycle your customer will actually use

Body fusing panels are worth watching especially closely, since a full-front chest piece covers a large, visible area where any mismatch shows immediately. This is why shrinkage compatibility between the interlining and your shell fabric matters more than the interlining’s shrinkage in isolation. A pair that each moves by a similar amount, in a similar direction, will fuse and hold its shape. A pair that moves at different rates is where rejects come from, usually discovered only after cutting, fusing, and sometimes after the garment has already shipped.

How to Pre-Test a Fusible Interlining Batch

The goal of a pre-test is simple: fuse a sample the same way you’ll fuse the bulk order, then put it through the same finishing or care process your garment will see, and check what moved.

This is general industry practice, not a specification tied to any one supplier, you should run it against your own press settings and your own shell fabric.

  1. Cut swatches from the actual roll of fusing cloth you plan to use, not from an old sample card. A batch pre-test only means something if it tests the batch you’re about to cut.
  2. Mark reference measurements before fusing. Draw a square or grid on the swatch (a 10cm x 10cm box works well) so you have a fixed, measurable baseline in both directions.
  3. Fuse the swatch using your actual production settings, the same press temperature, pressure, and dwell time you use on your shop floor, not a generic default.
  4. Let it cool fully and flat before measuring, and check the bond itself: no bubbling, no edge lifting, an even, consistent adhesion across the panel.
  5. Re-measure the marked square and record any dimensional change in both length and width.
  6. Run the swatch through your garment’s expected finishing or care process, washing or dry cleaning, using the same cycle the finished garment will go through, then measure again.
  7. Fuse a matching swatch of your shell fabric through the same steps and compare the two results side by side. What matters is the gap between them, not either number alone.
  8. Repeat across a few points in the roll, not just one cut, to see whether the batch is consistent from end to end.

Keep the results on file. A short record, swatch source, press settings, before-and-after measurements, and the shell fabric comparison, turns this from a one-off check into a repeatable step your team can run on every new delivery.

What to Check Before Starting Full Production

A pre-test only pays off if the results actually change a decision. Before you release a batch to bulk cutting, check:

  • Dimensional change is within what your garment construction can tolerate, compared against your shell fabric’s own movement
  • The bond held cleanly, no bubbling, delamination, or uneven adhesion on the test swatch after fusing and after washing or dry cleaning
  • Hand-feel and appearance are consistent across the swatches you tested from different points in the roll
  • The batch matches what you ordered, GSM, color, and construction consistent with previous deliveries of the same product
  • Results are compared against the specific shell fabric for this order, not a general assumption from a previous style
  • The test reflects your actual press settings and care instructions, not a generic lab default that doesn’t match your factory floor

If a batch passes on all of these, it’s ready for full production. For heavy, full-front body fusing especially, it’s far cheaper to catch a problem on a swatch than after a full run of panels has already been cut and fused.

Why Choose Double Ghoda for Fusible Interlining

Batch pre-testing works best when your supplier’s own process supports consistency in the first place. That’s something we take seriously: uniform GSM, hand-feel, and shrinkage across every delivery, so when you reorder from the same quality lot, you get the same product performance every time.

That consistency matters directly to the pre-testing process above. If a supplier’s deliveries vary widely from batch to batch, a pre-test result from one roll won’t tell you much about the next one, every new delivery becomes an unknown you have to test from scratch. When we keep our deliveries consistent, your pre-test results stay representative of the batches that follow, which helps your sourcing and quality team decide how often you actually need to re-test.

We also measure and verify every roll before dispatch, which matters for your production planning even beyond shrinkage. On fusing performance, our woven fusing cloth uses PA double-dot coating, a staggered two-coat adhesive pattern that gives faster, more even fusing and stronger resistance to delamination, which is directly relevant to how cleanly your panel bonds during the pre-test steps above. Our woven interlining is also dry-clean safe and OEKO-TEX® Standard 100 certified, and our range covers both woven and non-woven grades across a wide GSM band for different garment parts.

None of this replaces running your own pre-test on your own batch, press, and shell fabric. But when you source from a supplier that treats consistency as a stated priority, and you verify it yourself with the steps above, you cut down the number of surprises a new delivery can bring to your production floor.

FAQs

Does interlining shrink during fusing?

Yes. It can shrink or change dimensions slightly during fusing and again during washing or dry cleaning. The amount varies by construction and batch, which is why we recommend pre-testing a sample before full production.

What causes interlining shrinkage?

Heat and pressure from the press can relax residual tension in the base fabric, and moisture from later washing or dry cleaning can cause a further small dimensional change. Fiber type, coating, and batch-to-batch variation all play a role.

How do I pre-test a batch before production?

Cut swatches from the actual roll, mark a measured grid, fuse them using your real press settings, cool and measure, then run them through your garment’s expected wash or dry-clean cycle and measure again. Compare the results against a swatch of your shell fabric tested the same way.

Why does shrinkage compatibility with the shell fabric matter?

What causes problems isn’t dimensional change on its own, it’s a mismatch between how much the interlining moves and how much your shell fabric moves. A close match holds flat; a mismatch shows up as bubbling, puckering, or distorted seams.

What should I check before bulk production?

Confirm the dimensional change is within tolerance against your shell fabric, the bond held cleanly with no bubbling or delamination, hand-feel is consistent across the roll, and the batch matches your previous order’s specification.

Is batch-to-batch consistency the same as zero shrinkage?

o. Consistency means each delivery behaves the same way as the last one, not that there’s no dimensional change at all. Sourcing from a consistent supplier makes your pre-test results more reliable predictors for future batches, it doesn’t remove the need to test each new delivery.

Link of related Articles

shweta-textile-designer
 
Shweta, a textile designer with a keen eye and deep knowledge of fabrics, translates her passion into unique designs. She loves to share her expertise and ignite a love for textiles in others. Dive into the world of fabrics with Shweta!

Categories
Fusible Interlining Interlining

Interlining Fabric Shade Consistency in Bulk Orders

A bulk order that looks fine on paper can still cause trouble on the cutting table. Shade variation between rolls is one of the most common, and most preventable, problems in wholesale interlining supply. Here’s what shade consistency means, why it slips between batches, and what to check before you sign off on a large order.

Table of Contents

  1. Why Shade Variation Happens Between Batches
  2. What a Mismatched Batch Does to the Finished Garment
  3. What to Check Before You Accept a Bulk Order
  4. How Double Ghoda Keeps Shade Consistent Across Bulk Rolls
  5. FAQs on Interlining Fabric Shade Consistency

Why Shade Variation Happens Between Batches

Dye lot variation, roll-to-roll cutting differences, and storage conditions are the three main causes.

Dye lot variation is the biggest driver. Every dye bath run by a mill produces a slightly different depth of shade, even when the recipe on paper is identical. If two rolls of fusible interlining are drawn from different dye lots, even from the same supplier, on the same order, a visible colour difference is possible. This is a known, expected variable in textile dyeing, not a defect unique to any one factory.

Roll-to-roll variation can also show up within a single dye lot, usually from uneven dye penetration at the edges of a batch, or from rolls stored at different points in a warehouse for different lengths of time. Rolls cut from the start of a dye run and rolls cut from the end of the same run can carry a very slight difference in depth of shade, even though both are technically from one lot, this is why checking a few rolls from across a delivery matters more than checking just one.

Storage conditions matter more than most buyers assume. Rolls kept near heat, direct sunlight or high humidity for extended periods can shift tone slightly compared to rolls stored under stable, dry conditions. This is why roll to roll consistency depends as much on how a supplier stores stock as on how it was dyed.

None of this means bulk interlining sourcing is unreliable. It means shade needs to be checked as a routine step, not assumed.

There’s also a practical, unavoidable factor: base fabric and yarn can carry small batch-to-batch differences even before dyeing starts, which affects how evenly a dye lot takes colour. Mills manage this with shade-band tolerances, but a tolerance band still allows for some visible movement between the lightest and darkest roll in a run. A buyer who understands this treats shade checking as normal trade practice, not a sign something has gone wrong.

Coating can play a secondary role too. On woven grades with a PA double-dot finish, the coating itself doesn’t usually shift base shade, but a heavier or uneven coat can slightly change how light reflects off the surface, which sometimes reads as a tone difference even when the underlying dye lot is identical. It’s worth ruling this out before assuming a shade issue is a dyeing problem.

Interlining Fabric

What a Mismatched Batch Does to the Finished Garment

It shows up as visible shade lines, uneven fronts, and rejected pieces, after the fusing is already done.

A visible shade line under the lining of a sherwani front is the classic failure point. Buyers rarely spot it before pressing, and by the time the fusing cloth is bonded to the fashion fabric, the panel can’t be swapped without unpicking the whole front.

On blazers and suit jackets, a mismatched roll usually surfaces as one front panel reading slightly warmer or cooler than the other, visible mainly under bright showroom or daylight conditions, exactly where a finished garment gets inspected before it ships.

The downstream cost is what makes this expensive. A mismatched batch means reworked panels, delayed dispatch, and in the worst case, a full reject of finished pieces that already carry labour cost. For a factory running hundreds of pieces through cutting and fusing tables in a day, catching the issue at the roll stage is far cheaper than catching it at the finishing stage.

There’s a quieter cost too, buyer trust. A wholesale brand that receives even a small number of pieces with a visible shade issue tends to inspect the next order more closely, which slows down approvals and payment cycles on future purchase orders. For a factory supplying formal-wear brands at scale, a clean shade record across deliveries is part of what keeps repeat orders moving without added scrutiny.

Rework itself isn’t always straightforward either. Once a panel is fused, separating the base fabric from the interlining without damaging either layer is difficult and often not worth attempting, most factories simply cut a fresh panel from correctly matched material and treat the mismatched piece as waste. That waste includes the fashion fabric, not just the interlining, which is why the real cost of a shade issue is usually higher than the price of the roll that caused it.

What to Check Before You Accept a Bulk Order

Check rolls against a reference sample, under real light, across the full pallet, not just the top roll.

Use this as a quick pre-acceptance checklist:

  • Ask for the dye lot or batch reference on the delivery note, and confirm it matches your approved sample.
  • Compare against a physical reference swatch, not a photo or screen image, screens don’t render shade accurately.
  • Check under two light sources, daylight and a warm indoor light, since some shade differences only show under specific lighting (a known phenomenon called metamerism).
  • Inspect rolls from different points in the pallet, not just the top one. A shade shift can appear midway through a delivery.
  • Unroll a length from each roll, not just the outer wrap, since the outside of a roll can weather differently in storage than the inside.
  • Reorder against the previous lot when repeating a quality, request written confirmation that the new delivery is matched to your last approved batch, not just the same GSM and colour name.
  • Keep a physical swatch library of past approved batches on file at the factory, so intake staff have something fixed to compare against instead of relying on memory.
  • Flag issues before cutting starts, not after. A shade concern raised at intake can usually be resolved with the supplier before production begins; one raised after fusing rarely can.

This matters most for factories sourcing interlining fabric wholesale for repeat production, where every reorder has to match the last one already on the cutting table. A basic quality check at intake, done consistently, catches most shade issues before they reach the fusing press.

None of these checks need special equipment. A trained intake person, a reference swatch and two light sources cover most of what a factory needs to catch a shade problem before it reaches production. The habit matters more than the tooling, factories that skip this step under time pressure are the ones most likely to discover a mismatch late.

How Double Ghoda Keeps Shade Consistent Across Bulk Rolls

Batch-to-batch consistency is built into how we supply woven and non-woven interlining: uniform GSM, hand-feel and shrinkage across every delivery, so when you reorder the same quality lot, you get the same product performance every time.

Every roll of body fusing is measured and verified before dispatch on our end, which removes the short-metre problem that causes real production losses across this trade, a separate issue from shade, but one we check at the same intake stage.

For sherwani-scale orders, our 111 quality (140 GSM) remains the flagship fusing cloth grade, the one Surat buyers ask us for by name for full-front construction on heavy ethnic formal wear.

All our woven interlining fabric is OEKO-TEX Standard 100 certified and held in ready stock at our Bhiwandi, Maharashtra warehouse, with regular dispatch to Surat, Delhi, Ludhiana, Kolkata and Chandigarh. If you’re reordering, referencing your previous quality and quantity when you contact us helps us match the new roll to what’s already on your factory floor.

Ready stock also works in your favour on shade. Rolls that move faster through our warehouse spend less time in storage before dispatch, which limits the window for the kind of storage-related tone shift we covered earlier. If you’re placing repeat wholesale orders through the season, that turnover is as much a part of consistent supply as the GSM and coating specification on the roll itself.

FAQs on Interlining Fabric Shade Consistency

Can shade variation happen even within the same dye lot?

Yes, though less often. Uneven dye uptake at roll edges, or rolls stored under different conditions after dyeing, can produce a slight tone shift within one lot. It’s less common than lot-to-lot variation but worth checking for on large orders.

Does storage time affect the shade of a fusing roll?

Yes. Rolls held for long periods, especially near heat or direct light, can shift tone slightly compared to fresher stock from the same original dye batch. This is one reason ready-stock suppliers with fast turnover tend to show less variation.

Is a small shade difference always a defect?

Not always. Minor differences that are only visible under close, direct comparison may fall within normal trade tolerance. The problem is variation visible under standard inspection conditions or on the finished, pressed garment.

Should I request a batch reference on every bulk order?

Yes, particularly for repeat orders. A batch or dye lot reference lets you confirm a new delivery matches your last approved roll, rather than relying on the GSM and colour name alone.

Who should check for shade consistency at the factory, cutting staff or quality control?

Ideally quality control, at intake, before the roll reaches the cutting table. Cutting staff are focused on panel layout and yield, not shade comparison, so a mismatch is more likely to be caught early when a dedicated intake check is part of the process rather than left to whoever handles the roll first.

Link of related Articles

shweta-textile-designer
 
Shweta, a textile designer with a keen eye and deep knowledge of fabrics, translates her passion into unique designs. She loves to share her expertise and ignite a love for textiles in others. Dive into the world of fabrics with Shweta!

Categories
Fusible Interlining Interlining

How to Choose the Right Interlining Fabric for Different Garments

If you’re sourcing fusible interlining for a garment factory, the short answer is this: match the construction (woven or non-woven) to the garment part, then pick the GSM based on how much structure that garment needs. Full-front suits, blazers and sherwanis need heavier woven grades. Collars, cuffs and smaller parts do fine with lighter non-woven grades. Get these two decisions right and the rest of the sourcing process roll length, width, colour falls into place.

That’s the quick version. Below, we walk through how to apply it to your own production line, garment by garment.

Table of Contents

  1. Why Choosing the Right Interlining Matters
  2. Woven vs Non-Woven Interlining: Which One Is Right?
  3. How to Choose Interlining for Different Garments
  4. Choosing the Right GSM for Your Garment
  5. Common Mistakes When Choosing Interlining Fabric
  6. How to Select the Right Interlining for Bulk Production

Why Choosing the Right Interlining Matters
Interlining sits between the outer fabric and the lining. You never see it, but you feel its effect every time you pick up a jacket or sherwani and it holds its shape rather than collapsing in your hands.

Get the choice wrong and problems show up fast. Too light a grade under a suit front, and the chest looks flat after a few wears. Too heavy a grade on a collar, and it turns stiff instead of crisp. Neither looks good, and neither is easy to fix once the garment is cut and fused.

For garment manufacturers running bulk production, this isn’t a one-time decision, it’s one you’re making across every SKU and every season. A mismatch on one style can mean rejects, rework, or a customer sending pieces back. Getting the construction and weight right at the sourcing stage saves that cost later.

This also matters more in India than in many other markets. Indian ethnic formal wear, sherwanis, bandgalas, achkans, typically needs a heavier, firmer structure than international ready-to-wear, so sourcing decisions here don’t always match an international buying guide.

Interlining Fabric

Woven vs Non-Woven Interlining: Which One Is Right?

This is the question we hear most often from garment manufacturers and sourcing teams. In Surat’s trade language, this material is often called fusing cloth, but the real decision is woven versus non-woven, woven for the garment body, non-woven for smaller construction parts.

Woven interlining is a true woven fabric, polyester yarns interlaced in both directions, coated with adhesive on one side. Because it’s woven, it has higher tensile and tear strength and holds its shape under stress. That’s why it’s the standard choice for full-front fusing on suits, blazers and sherwanis, where the garment must hold structure through wear and repeated dry cleaning.

Non-woven interlining is made by bonding polyester fibres together rather than weaving them. It’s lighter and more economical, and it’s the right call for collars, cuffs, plackets and pockets, parts that need support but not the same load-bearing strength as a full jacket front.

Here’s how the two compare on the properties that matter for sourcing:

PropertyWovenNon-Woven
ConstructionWoven polyester yarnsBonded polyester fibres
CoatingPA double-dotPES single-dot
StrengthHigh tensile and tear strengthModerate, sufficient for small parts
GSM range30–150 GSM30–82 GSM
Roll length50 metres90 metres
Width150 cm100 cm
ColoursWhite, Black, GreyWhite, Black
Fusing temperature125–145°CUp to 120°C
Typical useSuits, blazers, sherwanis (full front)Collars, cuffs, plackets, pockets

Most factories don’t choose one over the other, they order both. A sherwani, for example, uses the heavier woven grade for the body and the lighter, fibre-bonded type for the collar. If you’re placing a bulk order, it’s worth quoting both together rather than sourcing them separately.

How to Choose Interlining for Different Garments

Once you know woven versus non-woven, the next step is matching the grade to the specific garment. Here’s how it typically breaks down for the main categories garment factories work with.

Sherwanis and heavy ethnic wear. Bandgalas, achkans and sherwanis need full-front body fusing that holds a firm, structured shape, this is where the heaviest woven grades come in. Within this category, one grade has become a recognised trade name on its own: 111 quality, a 140 GSM woven interlining that’s become the standard reference point for sherwani fusing in Surat and across North India. If you tell a supplier you need “111 quality,” they’ll know exactly what you mean without further explanation.

Structured suits. Suit fronts need enough body to hold their shape at the chest and lapel without feeling stiff to the wearer. This calls for a mid-to-heavy woven grade, light enough to drape naturally, heavy enough to resist collapsing.

Blazers and formal jackets. Similar logic to suits, but blazers can sit slightly lighter depending on the outer fabric and how structured the house style is. Premium or heavily tailored blazers lean toward the higher end of the same range; standard blazers sit lower.

Collars, cuffs and shirt plackets. These parts need to hold a crisp edge and spring back into shape, but they don’t carry the structural load a suit front does. This is squarely non-woven territory, or the lightest woven grades where a bit more durability is needed.

Lighter garments and ladies’ ethnic wear. Waistbands, pocket areas and softer silhouettes call for lighter interlining, non-woven where economy matters most, light woven where you need more durability.

The pattern across all of these: heavier structure needs woven, lighter support needs non-woven, and the exact GSM depends on how firm you want the finished garment to feel.

Interlining

Choosing the Right GSM for Your Garment

GSM, grams per square metre, is the single most important number when you’re comparing interlining options. It tells you how much the fabric will weigh, and roughly how much structure it will add. Too low, and the garment feels underbuilt. Too high, and it feels stiff and boardy. Here’s a general reference range by application:

GSM RangeTypical Application
30–40 GSMUltralight reinforcement, sheer or delicate fabrics
40–60 GSMCollars, cuffs, plackets
55–70 GSMLight jacket parts, waistbands
80 GSMStandard blazer body fusing
100 GSMFull-front structured suit fusing
120–130 GSMPremium suits, bandgalas, heavy formal wear
140 GSMSherwani full-front fusing (111 quality)
150 GSMMaximum structure, heavily embroidered sherwanis, overcoats

A useful rule of thumb for Indian ethnic formal wear specifically: don’t assume the GSM that works for an international ready-to-wear jacket will work for a sherwani. Indian garment manufacturers consistently use heavier grades, often 100 GSM and above, because ethnic formal wear is expected to hold a firmer, more structured silhouette than Western tailoring typically calls for.

If you’re not certain which GSM fits your fabric and garment combination, the safest approach is to test on a small cut before committing to a bulk run. A supplier who works with Indian ethnic wear regularly should also be able to point you to the grade that matches your garment type from experience.

Common Mistakes When Choosing Interlining Fabric

A few sourcing mistakes come up repeatedly across garment factories, and most are avoidable with upfront checking.

  • Assuming heavier is always better. A heavier GSM doesn’t always mean a better result, it means more stiffness. Over-structuring a lighter fabric can make the finished garment feel unnatural.
  • Using suit-weight interlining on shirts or lighter garments. Full-body woven grades are built for suits, jackets and sherwanis, not shirt or trouser construction, the structure and hand-feel are wrong for that application.
  • Ignoring the coating-and-temperature match. Woven and non-woven grades fuse at different temperature ranges. Running the wrong grade through a press set for the other type leads to weak bonds or scorching.
  • Not checking roll length and width before ordering. Woven and non-woven rolls come in different lengths and widths. If your cutting layout assumes one and you receive the other, you’ll end up with more wastage than planned.
  • Treating every supplier’s GSM label as identical. GSM, hand-feel and bonding performance can vary between suppliers even at the same stated weight. If you’re switching suppliers mid-production, test a sample batch before committing the full order.
  • Skipping a fusing test before a bulk run. The only way to confirm a GSM and coating combination works with your specific outer fabric is to press a test panel and check the bond, no bubbling, no edge lifting, consistent adhesion.

Most of these come down to one habit: confirm specifications and test before placing a large order, not after.

How to Select the Right Interlining for Bulk Production

Choosing the right fusing cloth for one garment is one exercise. Choosing it for a bulk production run, where consistency across thousands of metres matters as much as the initial specification, is a different discipline. Here’s a practical process to work through before you place a bulk order.

1. List out every garment type in the run. A single order might include sherwanis, blazers and lighter ethnic pieces. Each may need a different construction and GSM, so don’t assume one grade covers the whole order.

2. Match construction to garment requirement. For each garment type, decide woven or non-woven based on whether that part needs full structural support or lighter reinforcement.

3. Confirm the GSM for each application. Use your reference range, but don’t guess, request a sample cut and press it against your actual outer fabric before finalising quantities.

4. Check the required roll quantity against your cutting layout. Know how many rolls you need at what length and width, so the order quantity lines up with your production plan.

5. Confirm specifications in writing before the bulk order goes in. GSM, construction, coating type, colour and roll length should all be confirmed with your supplier before dispatch, not assumed from a previous order.

6. Review the minimum order requirement. Wholesale interlining suppliers typically work on a minimum order quantity rather than small or single-roll purchases, factor this into your planning if sourcing multiple GSMs or colours in one run.

7. Plan for batch-to-batch consistency. If reordering the same specification across production cycles, ask your supplier how they maintain consistent GSM and hand-feel between batches, this matters more at scale, where small variation compounds across thousands of garments.

8. Confirm before you commit, not after production starts. Once a bulk order is cut and fused into garments, it’s difficult and expensive to correct a mismatch. A short confirmation step upfront is cheaper than rework later.

We work with sherwani manufacturers, suit makers and blazer factories across Surat and North India on this kind of bulk sourcing of fusible interlining, from the initial GSM decision through to consistent repeat supply. If you’re planning a production run and want help confirming the right grade for your garments, we’re happy to walk through the specifications with you.

Frequently Asked Questions

Do I need a woven or fibre-bonded grade for a sherwani?

Both, typically. The full-front body uses a heavy woven grade for structure, while the collar and smaller parts use a lighter, non-woven type.

What GSM should I use for a structured suit?

Suit fronts generally sit in the 100–130 GSM woven range, depending on how firm you want the chest and lapel to feel.

Can I use the same interlining for suits and shirts?

No. Suit-weight woven grades are built for full-front structure and are too heavy and stiff for shirt or trouser applications, which call for much lighter constructions.

How do I know if a GSM is right before placing a bulk order?

Press a test panel against your actual outer fabric and check the bond and hand-feel before committing to full production quantities.

Link of related Articles

shweta-textile-designer
 
Shweta, a textile designer with a keen eye and deep knowledge of fabrics, translates her passion into unique designs. She loves to share her expertise and ignite a love for textiles in others. Dive into the world of fabrics with Shweta!

ENQUIRE NOW